Waste Tire Recycling Line Company Offers Turnkey Tire Recycling Systems for Maximum Output
2026-09-17
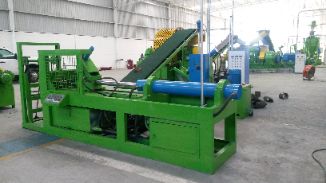
Some suppliers sell you a shredder and wish you luck. SFC takes a different route: we deliver complete turnkey tire recycling systems engineered for maximum output from the first run. Instead of piecing together equipment from multiple vendors, you get an integrated line built to convert whole waste tires into high-quality rubber crumb, powder, and clean steel—with minimal downtime and maximum material recovery. If you're ready to move beyond single machines and into serious production, this post breaks down what our turnkey approach actually includes and why it's changing the economics of tire recycling.
Turnkey Systems That Skip the Usual Startup Chaos
Most founders waste months stitching together payment processors, authentication flows, and admin dashboards before writing a single line of real business logic. Turnkey systems replace that entire phase with a pre-wired foundation—user accounts, billing, role permissions, and even basic analytics already working out of the box. You still own the code, but you skip the part where every startup rebuilds the same plumbing from scratch.
The real advantage isn't just saving time; it's avoiding the decision fatigue that kills early momentum. Instead of debating which database abstraction to use or how to structure webhook retries, a small team can focus on the one or two features that actually make customers stay. Turnkey platforms make opinionated choices for you, then get out of the way when you need to customize. The result is a launch that feels calm, not chaotic—your first user signs up on day ten, not day ninety.
That said, skip the term "turnkey" if it only means a pretty landing page with a login button. A true turnkey system handles the unglamorous edge cases: password resets that don't bounce, invoices that render correctly on mobile, rate limiting that doesn't lock out legitimate users. When those details are already solved, your team's energy goes into the product's actual differentiator, not the support tickets that would otherwise pile up in week one.
Output Isn’t Just Speed—It’s What Survives the Day
Many teams chase raw throughput—lines of code shipped, reports filed, tasks checked off—as if the number at 9 a.m. will carry the whole day. But by mid-afternoon, brittle work crumbles: a script needs patching, a decision made in haste gets reversed, an inbox full of quick replies spawns a longer thread of confusion. Enduring output isn't about how much you push out in hour one; it's about what still holds at hour seven.
Think of a kitchen during lunch rush. The fastest cook might plate forty dishes by noon, but if three come back for being undercooked and two sauces split, the speed is an illusion. The cook whose plates never return—slightly slower, maybe fewer—owns the day. That's the real metric: not units produced, but units that don't need rework. Real throughput is measured in survivor output, the kind that doesn't quietly become someone else's problem.
Building work that lasts a full day means resisting the urge to optimize for the first glance. It means adding a few seconds of verification now to avoid an hour of debugging later. It means leaving notes clear enough that no one pings you at 4 p.m. asking what you meant. Speed gets you a head start; durability gets you to the finish line.
How the Line Handles Steel, Fiber, and Rubber Together
Mixing steel, fiber, and rubber on one line isn't a simple handoff—it's a constant negotiation between rigidity and flexibility. Steel cord arrives in heavy coils that get straightened and cut to exact lengths before being laid into position. Fiber layers, whether polyester or aramid, are tensioned through rollers that prevent wrinkles and keep the ply angle consistent. Rubber compounds, still warm from mixing, are calendered into sheets that sandwich the other materials. The line's job is to make sure each layer bonds without trapping air or shifting under pressure.
The trick is in the timing and the tension. If the steel is fed too fast, it can slice through a fiber layer. If the rubber cools too much, it won't flow into the gaps between cords. Operators watch the accumulator loops and adjust the dancer rolls to keep every material moving at the same relative speed. Sensors check thickness and alignment, but experienced hands still tap the rubber to feel for soft spots where adhesion might fail later.
At the end, the layered composite passes through a series of pressure rollers that force the rubber into the cord spaces without crushing the fiber. The result is a single, continuous strip that holds its shape but can still flex under load. That balance is what the line is tuned for—steel for strength, fiber for stability, rubber for grip and weather resistance, all fused at the same pace.
Built for Truck Tires, Not Just Passenger Cars
Most tire reviews and buying guides focus on passenger cars, but truck owners face a completely different set of demands. Load ratings, sidewall stiffness, and heat dissipation under heavy payloads are not optional extras—they determine whether a tire survives a cross-country haul or fails on a job site. A tire designed for a sedan simply does not have the internal structure to handle a fully loaded pickup or delivery van, yet many generic recommendations ignore this distinction.
When you look closely at truck-specific tire construction, the differences go beyond tread depth. Reinforced bead areas, extra steel belts, and compounds tuned for high torque and towing stress separate a real truck tire from a passenger tire with an aggressive tread pattern. These are not marketing details; they show up in how evenly a tire wears, how stable it feels with a trailer attached, and how much heat it can shed before losing integrity.
Choosing truck tires means ignoring the one-size-fits-all advice that dominates quick searches. Instead, start with your actual load range, typical road surfaces, and whether you need highway, all-terrain, or mud-focused performance. That approach keeps you from ending up with a tire that looks tough but gives out exactly when you need it most.
When Maximum Output Meets Minimum Downtime
Running a production line at full tilt while keeping unscheduled stops to a near-zero level sounds like a contradiction until you watch a well-tuned operation in action. The trick isn't pushing every machine to its breaking point; it's recognizing that small, deliberate pauses for inspection and adjustment actually protect the longer stretch of continuous output. Teams that master this balance treat downtime not as an enemy to be eliminated, but as a resource to be spent wisely on the right components at the right moment.
The real leverage comes from shifting attention away from heroic, last-minute fixes and toward the quieter work of watching for faint signals. A slight rise in vibration, a subtle drop in hydraulic pressure, or an unusual pattern in energy draw can all point to a failure that hasn't happened yet. When operators have the authority to act on those readings immediately, a ten-minute intervention often prevents a ten-hour stoppage. That kind of responsiveness doesn't slow the line down; it smooths out the jagged peaks and valleys that quietly eat into annual throughput.
In the end, the operations that stand out aren't the ones running blind at maximum speed until something breaks. They're the ones that treat every shift as a loop: measure, adjust, verify, repeat. By making small stops predictable and purposeful, they create a rhythm that looks almost lazy from the outside but consistently delivers more finished units per week than a frantic, breakdown-plagued rival. It's not about doing less. It's about making every minute, including the ones spent not running, count toward the same goal.
From Waste Tires to Consistent, Salable Material
Mountains of discarded tires have long been an eyesore and a fire hazard, but they also hold a surprisingly uniform raw material. The rubber, steel, and fiber inside a tire are not random scraps; they come from precise manufacturing standards. When a processing line shreds, granulates, and separates these components, the resulting crumb rubber or steel wire can be remarkably consistent batch after batch. That consistency is the first step toward turning a disposal problem into a product buyers actually want.
The key is controlling the shredding and screening stages. Instead of simply crushing tires into jagged chunks, a well-tuned line uses multiple reduction steps with magnetic separation for steel and air classification for fiber. Each pass narrows the particle size distribution, removes contaminants, and stabilizes moisture content. Over time, operators learn to adjust rotor speed and screen size to hit a narrow specification—say, 10–20 mesh rubber with less than 0.5% fiber. That repeatability makes the output predictable, which is what manufacturers of molded goods, playground surfaces, and rubberized asphalt require.
Once the material meets a tight spec, it stops being “waste” and becomes a commodity. Buyers do not want surprises in density, metal content, or color. A processor who can supply truckload after truckload of the same rubber powder or clean steel wire builds trust quickly. That trust allows the material to flow into existing supply chains without special handling or blending. The difference between a tire pile and a salable product is not magic—it is steady, measurable consistency backed by honest quality checks.
FAQ
Everything from initial shredding and steel separation to fiber removal and final granulation. The company handles layout, equipment supply, installation, and operator training so the plant is ready to run.
It depends on the configuration, but most systems are designed to process between 500 kg and 3 tons of tires per hour. Higher throughput is possible with additional shredders and screens.
Not really. The control panel is straightforward, and the cutting tools are built for quick replacement. Daily checks take less than 15 minutes, and most wear parts last several hundred hours.
Whole passenger car and light truck tires can go directly into the primary shredder. For larger tires like tractor or mining tires, a simple debeading step is recommended to avoid jamming.
The main outputs are clean rubber granules, steel wire, and textile fiber. The rubber can be sold for playground surfaces, sports tracks, or molded products, while the steel goes to scrap metal buyers.
From delivery to full production usually takes two to four weeks, depending on the plant size and site preparation. The company sends a team to supervise assembly and run initial tests.
Yes, they provide remote troubleshooting, spare parts delivery, and optional on-site service visits. Many customers also get a first-year maintenance package included with the purchase.
Conclusion
Setting up a tire recycling operation often means months of fine-tuning separate shredders, granulators, and classifiers. This company changes that with turnkey systems that arrive pre-engineered to work as one line from day one. Instead of wrestling with startup chaos, operators get a process where steel, fiber, and rubber are pulled apart cleanly at each stage. The result is not just a fast first hour—it's an output that holds up over a full shift. Rotors stay balanced, screens don't clog, and the material keeps flowing even when feed size varies.
What really sets the line apart is that it's built for truck tires and other heavy casings, not just passenger car scrap. That means the infeed, shredding, and separation stages are sized for thick sidewalls and high-tensile bead wire. Downtime stays low because wear parts are easy to reach and replace without tearing down the whole system. The end product comes out as consistent, salable rubber granulate or powder, free of loose steel and fluff. For a processor that needs maximum output every day, this kind of turnkey setup removes the guesswork and keeps the line running.
Contact Us
Contact Person: Chen Zhengwei
Email: [email protected]
Tel/WhatsApp: +86-13963975727
Website: https://www.sfcrubbermachine.com