Ultrasonic Coating System Vendor: How to Choose the Right Partner for Precision Thin-Film Applications
2026-09-27
Most ultrasonic coating system vendors will show you a clean spec sheet; far fewer will show you how their equipment holds up when coating ultra-thin, defect-sensitive films at production speed. If you're evaluating partners for precision thin-film applications, the difference isn't in the brochure—it's in the process control, repeatability, and support behind the nozzle. Here's how to separate genuine expertise from sales talk, and why Siansonic is often part of the shortlist.
Start with the Fluid, Not the Machine
Most people reach for the machine first—the framework, the tool, the rigid process—and then wonder why the result feels hollow. The fluid is what actually moves: the idea, the emotion, the data, the conversation. When you begin there, the machine becomes nothing more than a container shaped around something that was already alive.
Think of a river before a dam. The water doesn't ask permission to flow; it finds every crack, every gradient, every path of least resistance. If you start by designing the dam without watching the water, you'll build in the wrong place. But study the fluid long enough, and the structure almost suggests itself—curves, pressure points, spillways, all dictated by behavior rather than assumption.
This shift is uncomfortable because it asks you to tolerate mess before method. Fluids are unpredictable. They leak, swirl, change phase. But that unpredictability carries the exact information you need. Let the fluid run long enough to see its patterns, and the machine you eventually build will feel less like an invention and more like an acknowledgment of what was already trying to happen.
Ultrasonic Nozzle Specs That Predict Coating Quality
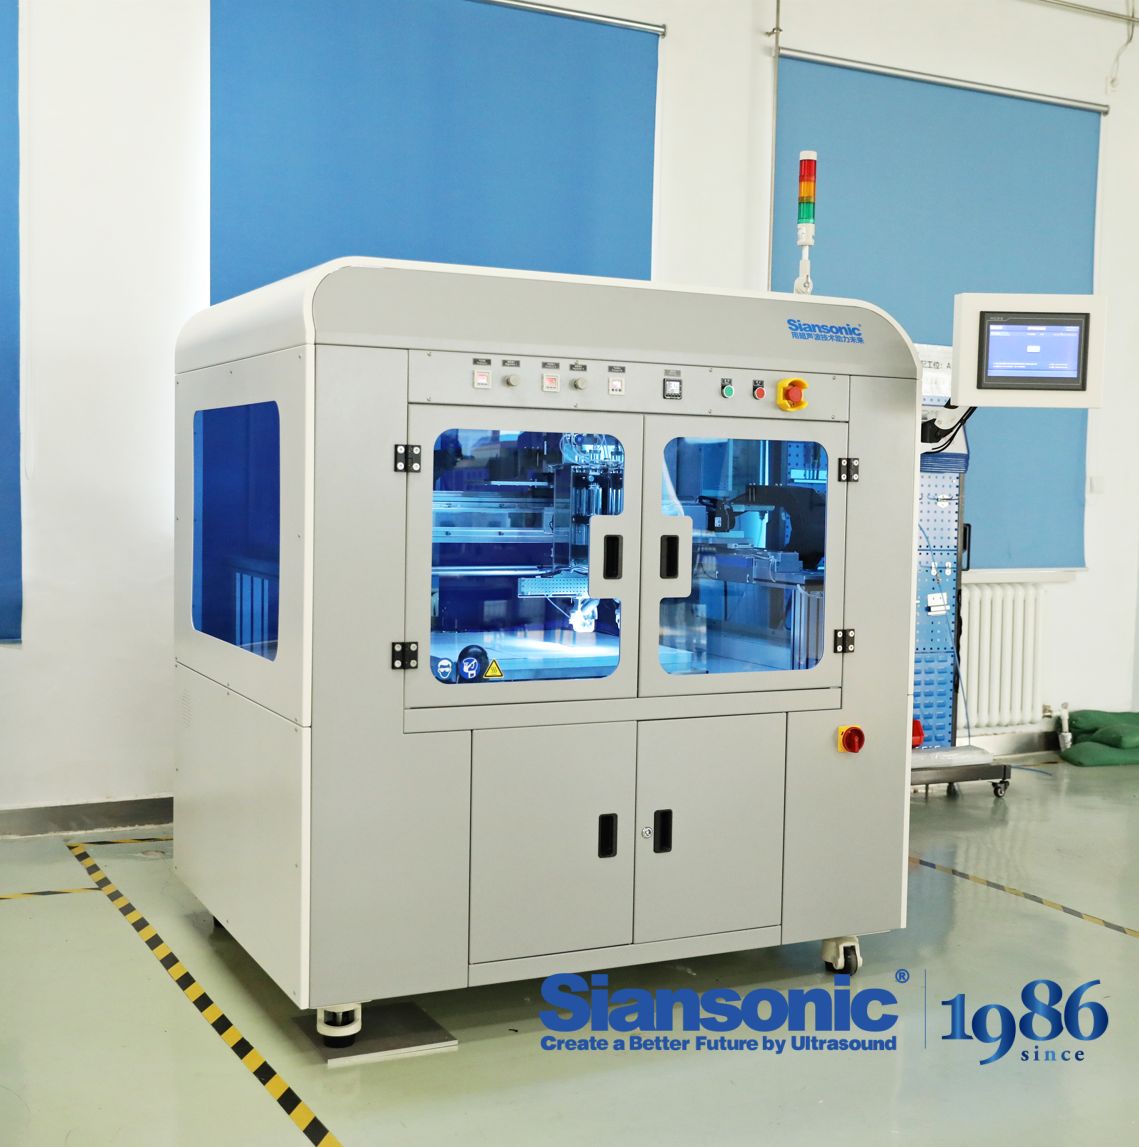
Frequency alone rarely tells the whole story, but it is the spec that most directly shapes droplet size. A 48 kHz nozzle can atomize low-viscosity coatings into a fine mist, yet the median droplet diameter often jumps when viscosity climbs above 30 cP. That shift matters because larger droplets settle unevenly, creating streaks and uneven film build. Pairing the frequency with the nozzle's orifice diameter gives a better read. For a 100 µm orifice at 60 kHz, you can expect a relatively narrow plume that favors precise edge definition on small parts. The same frequency with a 200 µm orifice tends to widen the spray angle and increase throughput, but at the cost of a coarser finish if the coating has any shear-thinning behavior.
Flow rate and liquid pressure are equally telling, especially when cross-checked against the nozzle's published turndown range. A nozzle that specifies a minimum stable flow of 5 ml/min will not produce a clean, continuous film if you push it to 2 ml/min; the spray starts to pulse, and that pulsing leaves visible banding. The maximum amplitude setting also has a threshold beyond which cavitation inside the liquid path generates microbubbles. Those bubbles pop on the substrate and leave tiny pinholes, a defect that is often blamed on coating chemistry rather than nozzle setup. Checking the amplitude spec against the coating's boiling point and dissolved gas content can prevent that issue before it appears on the line.
Spray pattern dimensions come from the nozzle body geometry and any air-shaping cap, not from the transducer alone. A wide, flat pattern works for large panels but makes it hard to keep wet film thickness consistent near the edges. A conical pattern from a focused nozzle tends to deliver a thicker center and thinner rim, which can be corrected by adjusting the nozzle-to-substrate distance only within a narrow window. If the datasheet lists a Sauter mean diameter of 15–20 µm at a given flow, that is a stronger predictor of coating smoothness than the nominal power rating. Consistently hitting that droplet size across the full flow range is what separates a nozzle that merely sprays from one that actually controls film quality.
Scaling from Benchtop to Production Without Losing Uniformity
Moving a process from a benchtop setup to full production rarely fails because the chemistry changes—it fails because the physical environment changes in ways that quietly undermine uniformity. On the bench, a small vessel gives you nearly instant thermal equilibration, predictable mixing, and easy manual intervention. In a pilot or production reactor, those assumptions collapse. Temperature gradients appear across the bulk, agitator tip speeds shift the shear profile, and surface-to-volume ratios alter how quickly heat and mass transfer happen. Uniformity isn't lost in a dramatic event; it erodes through slower, less obvious mismatches between what worked in a flask and what actually happens in a 2,000-liter vessel.
The practical fix is to treat scale-up as a translation problem rather than a simple multiplication. Instead of blindly holding stirring speed or batch time constant, map the bench process to dimensionless parameters like mixing time, power per unit volume, or Reynolds number—then deliberately test the boundaries of that map at intermediate scales. Use inline particle size or viscosity measurements to spot the first signs of non-uniformity before they become off-spec product. And resist the urge to "fix" a scale-up issue by adding more mixing energy alone; sometimes the better lever is changing raw material addition sequence, seeding strategy, or even the geometry of baffles. Uniformity survives scale-up when you maintain the same local micro-environment a molecule or particle experiences, not when you replicate the lab recipe by rote.
What a Vendor's Defect Library Reveals About Experience
A vendor's defect library is far more than a running list of past mistakes. It maps how the team has encountered, diagnosed, and stabilized real-world failures over time. The depth of each entry—root cause notes, environmental triggers, fix rationale, regression risk—shows whether the vendor treats defects as isolated incidents or as opportunities to harden the product.
Experienced vendors tend to organize defect data in ways that speed up future troubleshooting. You'll see recurring failure signatures linked to specific components, release conditions, or customer workloads. Less mature teams often log only the symptom and patch, leaving no trail for understanding why a problem resurfaced. That contrast reveals how much institutional knowledge actually sits behind the code.
Reading a defect library with a critical eye can uncover whether a vendor has dealt with edge cases, long-tail integration issues, or performance degradation under stress. A sparse or vague library doesn't necessarily mean a flawless product—it often means the team hasn't been forced to confront hard problems yet. The real signal is not the number of defects, but the quality of learning embedded in each record.
Support Questions to Ask Before You Sign
Before you sign anything, push for clarity on how support actually reaches a human. Does the vendor assign a dedicated contact or shuffle you through a shared inbox? Ask whether phone support costs extra or is bundled into the fee, and what a realistic response window looks like during business hours versus late on a Friday.
Escalation paths matter more than the initial answer. If a support rep can't resolve the issue, how long until someone with real authority steps in? You need specifics on senior engineer availability and whether there's a bypass for critical outages. Otherwise, you might find your production system down while you wait for a callback that never comes.
Don't skip the fine print on support limits. Are there monthly caps on tickets? What about help with custom integrations or after-hours emergencies—are those treated as extra billable work? Get every promise in writing, because a salesperson's reassurance won't hold up when you're arguing over an invoice.
Process Data to Demand from Every Coating Trial
Most coating trials get reduced to a simple pass/fail note, but that wastes most of what the run can tell you. Every trial is a dense record of variables—ambient temperature, humidity swings, mixing time, spray pressure, flash-off interval, oven ramp rate, final film thickness. If you only log whether adhesion looked okay, you miss the small shifts that will bite you later on a different line or in a different season. Start by capturing the conditions as they actually happened, not as the spec assumed they would.
Once the raw numbers are in hand, force them into a shape that lets you ask sharper questions. Normalize the viscosity readings to a common temperature, flag any thickness outlier before it skews the average, and plot cure temperature against crosshatch adhesion or salt spray hours. You don't need a data science team—simple scatter plots and honest note-taking often expose a pattern, like longer flash-off times improving gloss only below a certain humidity threshold. Each of those patterns should be turned into a demand: change the induction time, tighten the substrate roughness band, adjust the activator ratio by 2 percent.
Finally, make the trial output feed the next experiment instead of sitting in a folder. Turn every observation into a concrete next-step instruction and hand it to the formulator or line operator the same week. Over a dozen trials, those demands accumulate into a living process definition that no single lab study could have produced. That's the real point of processing data from every coating trial—not to prove the coating worked, but to build a body of evidence that tells you exactly what to demand from the next one.
FAQ
Look beyond brochure specs. Ask for actual coating thickness maps from a test run with your fluid, not a generic demo. Check whether the vendor controls droplet size distribution through nozzle frequency and surface tension matching, and whether they offer in-situ thickness monitoring or at least a clear calibration procedure. A vendor that can discuss edge bead suppression and drying dynamics alongside the hardware is usually the safer bet.
Probe their application notes. Ask about specific thin-film challenges like coffee ring effects, pinhole formation, or viscosity drift during long runs. A specialist will share concrete examples of solving those issues with parameters like standoff height, flow rate ramping, or temperature control. If they pivot to generic features like 'high uniformity' without explaining how it is achieved under your process window, treat that as a warning sign.
Request a structured feasibility study that includes viscosity and surface tension measurements of your formulation, a design of experiments on key variables (flow rate, head speed, ultrasonic power), and a final coating report with thickness data across the substrate. The report should include failure modes they observed, not just the best run. If they refuse to share raw data or only show one perfect sample, keep looking.
The nozzle determines how uniformly the ultrasonic energy is delivered and how stable the spray cone remains over time. Ask about the nozzle material's compatibility with your solvent, whether the tip can handle continuous operation without clogging, and how the vendor controls droplet velocity. A narrow, well-collimated spray pattern with low kinetic energy is essential for thin films on delicate substrates; otherwise you risk overspray, uneven wetting, or substrate damage.
Factor in solution waste during startup and shutdown, nozzle replacement frequency, cleaning solvent usage, and the time lost to manual recalibration. Ask for real-world data on uptime and mean time between failures for the specific nozzle model proposed. Also consider whether the vendor offers remote diagnostics or on-site service within a short window, because thin-film production stoppages can be far more expensive than the hardware itself.
A dedicated application lab signals that the vendor can iterate on your process quickly without tying up your own production line. You should expect to send them your fluid and substrate, then receive coated samples with full parameter logs. More importantly, ask if the lab team includes material scientists or chemical engineers who can interpret results, not just technicians running a script. The depth of that conversation often reveals the true value of the partnership.
They over-index on maximum coating width or throughput and ignore the smaller details that govern repeatability, like flow meter resolution, nozzle alignment fixtures, and environmental controls. Another frequent mistake is not testing the system with their actual production fluid in the same humidity and temperature range. That leads to surprises during scale-up. A good selection process includes a day-long pilot with the vendor's engineers observing your coating line, not just a sales demo.
Look at their track record with customers who started in R&D and later scaled to production. Ask for references where the vendor supported a transition from low-volume lab coating to continuous roll-to-roll or large-area coating. Also check whether they document software updates, offer training for new operators, and maintain a knowledge base for troubleshooting. A vendor that proactively tracks your process after installation and suggests improvements is more likely to help you avoid thin-film defects down the road.
Conclusion
Selecting an ultrasonic coating system vendor for precision thin-film work rarely begins with the hardware. It starts with your fluid. A capable partner will ask about viscosity, solids loading, surface tension, and solvent evaporation rates before recommending any nozzle. If a vendor jumps straight to machine specs, that is a red flag. Once the fluid is understood, look closely at the ultrasonic nozzle parameters: operating frequency, amplitude control, flow rate range, and the ability to maintain a stable spray cone. These details dictate droplet size distribution and ultimately film uniformity. Pay attention to how the vendor discusses scaling from benchtop to production. Many systems work fine at small scale but lose edge uniformity or coating thickness control when line speed increases or substrate dimensions change. The right vendor will have concrete strategies for maintaining the same acoustic energy per unit area across scales, not just vague promises.
Experience shows up in a vendor's defect library. Ask to see examples of common coating failures—overspray, drips, orange peel, pinholes, ribbing—and how they were resolved. A rich defect library demonstrates years of troubleshooting across different fluids and substrates. Before signing any agreement, probe their support model. How quickly do they respond to process upsets? Do they offer onsite training or remote diagnostics? Are replacement parts readily available? Finally, demand detailed process data from every coating trial. This means not just final film thickness but real-time records of flow rate, nozzle power, atomization pressure, substrate temperature, and any environmental conditions. Without that level of transparency, you cannot replicate results or diagnose future issues. Choosing a partner who treats process data as a deliverable rather than an afterthought will save months of frustration down the line.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/