Tris(2-ethylhexyl) Phosphate Factory Practices That Ensure High Purity and Safety
2026-10-19
When it comes to specialty phosphate esters, purity and safety aren’t just checkboxes—they’re the difference between a reliable supply chain and a costly recall. At Fortune, we’ve spent years refining our Tris(2-ethylhexyl) Phosphate (TEHP) manufacturing process to eliminate impurities that others overlook. But what actually happens inside a factory to guarantee both high purity and rigorous safety? In this post, we pull back the curtain on the specific practices—from raw material screening to final packaging—that set TEHP production apart. Whether you’re a formulator, procurement lead, or quality engineer, understanding these steps could help you avoid hidden risks and optimize your next project.
Incoming Phosphate Feedstock Gets Rejected Unless It Passes a 12-Point Purity Screen
Every incoming phosphate feedstock load sits at the receiving dock until its twelve-point purity panel clears. The checks aren't just for show—moisture, cadmium, arsenic, fluoride, silica, and acid-insoluble residue all get measured against tight thresholds. A single out-of-spec result rejects the entire truck, and the supplier eats the return freight.
The twelve-point screen runs in a fixed sequence, with duplicate samples drawn from three different depths inside the trailer. Lab techs log each result to the lot number before the discharge valve is unlocked. If any reading falls outside the band, the system automatically flags the shipment and triggers a resample; a second failure moves that supplier to probation.
This gatekeeping has changed how suppliers behave. Most now run their own pre-screening before dispatch, because a rejected load costs them time and credibility. Plant operators see fewer acidulation upsets and less unplanned downtime, which matters more than the occasional argument over a borderline silica reading.
Distillation Under Deep Vacuum Removes Residual Alcohols Without Cracking the Ester
Residual alcohols are a common byproduct in esterification reactions, and their removal often demands temperatures that push esters close to their thermal limits. Under deep vacuum, the boiling points of these lighter alcohols drop dramatically, so they can be stripped away at temperatures far below the point where the ester backbone begins to crack. This avoids the classic problem of sacrificing yield to unwanted acid-catalyzed decomposition or beta-elimination side reactions that occur during prolonged high-heat distillation.
The key is maintaining a vacuum level low enough—typically in the range of 0.1 to 5 mbar—to create a wide boiling point gap between the residual alcohol and the target ester. At these pressures, short-path or thin-film evaporators give the alcohol molecules a very short residence time in the heated zone. The ester sees only a brief thermal pulse, enough to let the volatile alcohol escape while the larger, heavier ester molecule remains intact. Cracking, which usually requires higher energy input to break the ester linkage, simply does not get the chance to occur.
Careful condenser design matters as much as the vacuum pump. The condenser must be cold enough to trap the stripped alcohol immediately, preventing it from re-entering the liquid phase and raising the partial pressure in the system. Many setups use a two-stage cold trap arrangement with the first stage slightly above the alcohol's freezing point and the second at much lower temperature. This keeps the vacuum steady and the separation clean, letting the ester come off the process at high purity with its chemical structure fully intact.
In-Process Acidity and Moisture Checks Every Four Hours Prevent Off-Spec Batches
A four-hourly sampling rhythm catches drift in acidity and moisture long before it can push a batch outside specification. Operators pull a small portion from the line, run a quick titration or moisture balance check, and record the values on the control chart. These two parameters rarely shift in isolation—when moisture climbs, acid ratios often follow, and the combination can ruin texture, shelf life, or reaction efficiency downstream.
The mid-shift checks create a narrow window for correction. If a reading comes in at the upper warning limit, the team adjusts dryer temperature, feed rate, or blending time immediately, rather than waiting for the final lot analysis. This prevents the familiar pattern where a full production run gets quarantined or reworked because a subtle change went unnoticed for eight or twelve hours.
Over multiple campaigns, the four-hour interval has proven to match the typical speed of process drift in this unit. Longer gaps allow too much material to accumulate between measurements, while shorter ones add lab workload without meaningful benefit. Keeping the checks tight but practical means fewer rejected batches, less rework, and a steadier output that meets both internal specs and customer expectations.
Sealed Sampling Ports and Glove Boxes Keep Operator Exposure Below 0.1 ppm
Operators rarely think twice about the air they breathe until a process demands near-zero contact with hazardous powders or solvents. Here, sealed sampling ports and glove boxes work as a quiet barrier. The ports allow material to be drawn out without breaking containment, while the glove boxes maintain a controlled atmosphere around every manual step. Together they keep ambient concentrations under 0.1 ppm, a threshold that only becomes noticeable when something is off.
What makes the setup practical is how it removes the need for constant PPE adjustments or rushed movements. A technician can reach into the box, open a sample vial, and seal it again without ever feeling air movement on the back of the hand. The sampling port locks after each use, so the line never stays open longer than necessary. Even during shift changes, the room monitoring shows a flat trace, not a spike.
Over time, the combination proves itself by the absence of alarms and the low frequency of filter replacements. It works because containment is built into the hardware rather than depending on operator memory. For any site handling potent compounds, that kind of passive reliability is the difference between a routine procedure and a recurring exposure report.
Stainless-Steel Transfer Lines Are Flushed with Dry Nitrogen After Each Run
Once a production cycle ends, the stainless-steel transfer lines don't simply sit idle. Crews run dry nitrogen through the entire network to push out residual product, moisture, and oxygen. This isn't a quick puff—it's a sustained flush that reaches every bend, valve, and connection point.
The choice of dry nitrogen matters because it's inert and leaves no residue. Unlike compressed air, nitrogen won't introduce humidity or react with trace chemicals left behind. That keeps the lines from corroding or forming deposits between runs, which is critical when switching from one product to another.
Operators track the nitrogen pressure and duration closely. A typical flush might last until sensors confirm the oxygen level inside the line drops below a set threshold. Only then is the system sealed and marked ready for the next product transfer.
Final Product Must Survive a 72-Hour Thermal Stability Challenge Before Shipping
The 72-hour thermal stability run is not a formality. Each finished unit gets placed in a programmable chamber that cycles between high and low extremes, often ramping from -20°C to 60°C over repeat loops. Engineers watch real-time telemetry for any drift in output, impedance, or seal integrity. A single deviation outside the accepted band is enough to stop the batch.
Why hold product for three full days? Shorter tests miss failures that only appear after sustained thermal stress. Solder joints can develop micro-cracks, adhesives may creep, and pressure seals can relax. By the time the 72-hour mark passes, those hidden weaknesses have either shown up or been ruled out with reasonable confidence.
There is no shortcut here. Every shipment goes through the same protocol, and the data log from each chamber run is archived with the lot number. If a unit fails, it is quarantined for root-cause analysis rather than being retested until it happens to pass. That hard gate is what keeps field returns low and customer trust intact.
FAQ
The alcohol feed (2-ethylhexanol) needs low moisture and carbonyl content because water can promote side reactions and carbonyls can create colored impurities. We also insist on low acidity in the alcohol to avoid catalyst poisoning, and we test every incoming lot with gas chromatography before it enters the esterification reactor.
Instead of running a single long batch, we use staged addition of phosphorus oxychloride and keep the temperature curve tight around 60–70°C. The unreacted HCl is swept out continuously with a dry nitrogen purge, and we monitor the acid number in real time. This prevents over-reaction and keeps mono- and di-ester impurities below 0.2% before neutralization.
After neutralization, we wash the crude ester with dilute alkali and then with deionized water at 60°C. A thin-film evaporator strips light volatiles, and a final vacuum distillation under 5 kPa removes heavy phosphate esters. We then pass the product through a 0.5-micron filter to eliminate any particulates.
The POCl3 feed is kept in sealed, double-walled storage with continuous moisture monitoring. Dosing is done under slight negative pressure, and the reactor area has both water spray curtains and dry chemical extinguishers because water on a large POCl3 spill can create a violent exotherm. Operators wear acid-resistant suits and use closed-circuit breathing air during any line opening.
We run three independent methods on every batch: gas chromatography for mono- and di-ester content, ion chromatography for chloride and phosphate ions, and Karl Fischer titration for water. The batch is only released if all three pass the internal limit, which is tighter than the customer specification. Retained samples are then stored for two years for traceability.
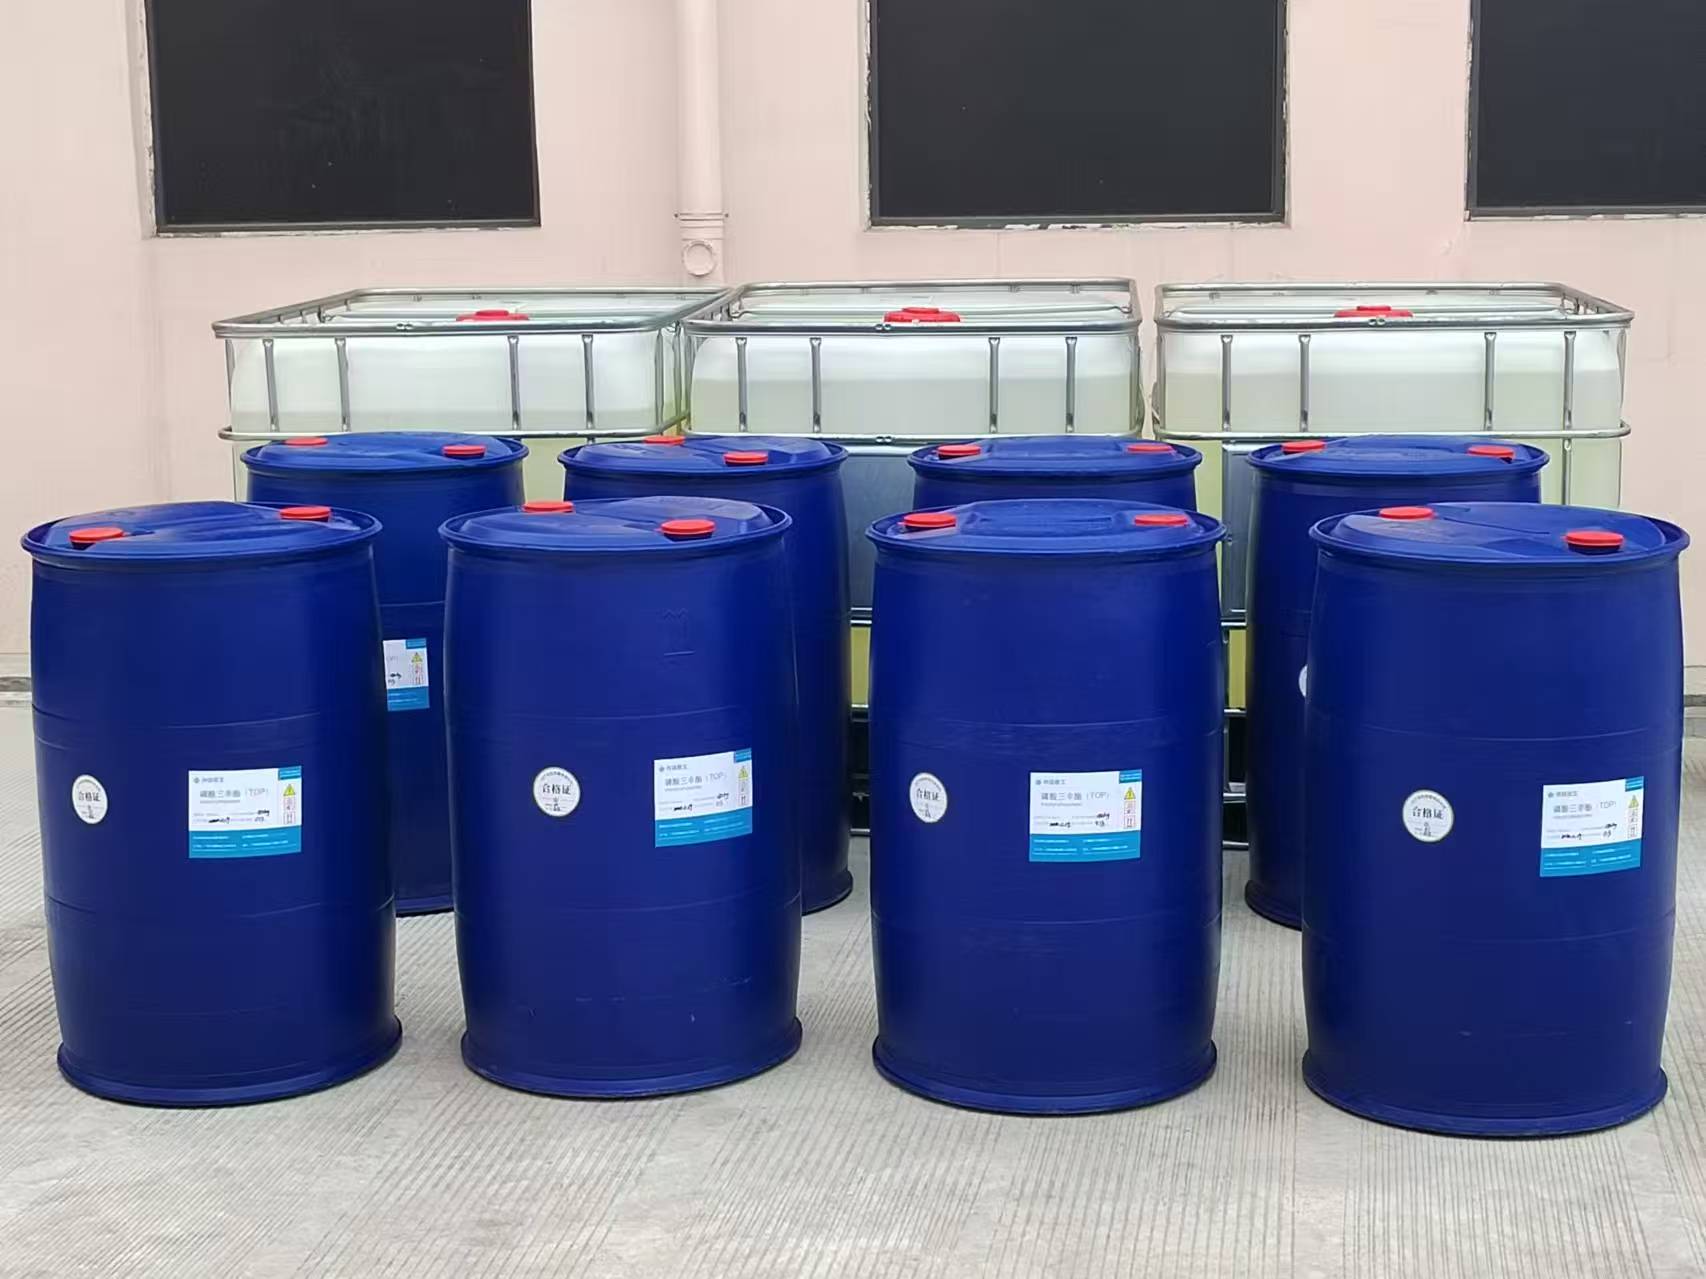
The finished ester is blanketed with nitrogen and filled into epoxy-lined steel drums or ISO containers. We avoid any exposure to air above 5% relative humidity during filling, and drums are stored indoors below 40°C. Each container gets a tamper-evident seal and a batch-specific COA with the exact impurity profile.
Yes. The HCl byproduct is scrubbed in a two-stage water absorber to make 30% hydrochloric acid for sale, which eliminates venting. The plant’s closed-loop cooling water and solvent recovery systems mean there are no open drains near the reactor. This reduces fugitive emissions and keeps the operator area consistently below 1 ppm for HCl, which is safer and cleaner.
Metals like iron and nickel can catalyze decomposition and color formation during storage or high-temperature end-use. We use glass-lined reactors and 316L stainless steel piping with electropolished surfaces, and we add a chelating agent during the water wash. Our ICP-MS check on every batch shows iron and nickel each below 0.5 ppm.
Conclusion
At the heart of this facility's operation lies a rigorous rejection system for incoming phosphate feedstock, which must clear a comprehensive 12-point purity screen before a single drum is accepted. This initial gatekeeping step eliminates contaminants that could otherwise compromise downstream quality. Once approved, the raw ester moves into a deep-vacuum distillation stage engineered to strip residual alcohols at low temperatures, preventing thermal cracking of the phosphate ester itself. Throughout each batch cycle, technicians perform acidity and moisture checks every four hours, using sealed sampling ports and glove boxes that keep operator exposure to airborne Tris(2-ethylhexyl) phosphate below 0.1 ppm—a threshold far stricter than common industry norms.
After distillation, stainless-steel transfer lines are purged with dry nitrogen following every run, effectively removing trace oxygen and humidity that could initiate degradation or corrosion. The finished product must then withstand a 72-hour thermal stability challenge under controlled elevated temperatures, with any sign of viscosity shift, acid number drift, or color change resulting in automatic quarantine. These interlocking practices—front-end screening, mid-process monitoring, closed handling, inert line maintenance, and end-point stress testing—form a quality architecture that prioritizes both chemical purity and worker safety, making the factory a benchmark for high-purity phosphate ester production.
Contact Us
Contact Person: WANG SIHAI
Email: [email protected]
Tel/WhatsApp: +86-13815295628
Website: https://www.fortunechemtech.com/index_en.html