Iron Casting Factory Processes That Deliver Unmatched Component Strength
2026-11-16
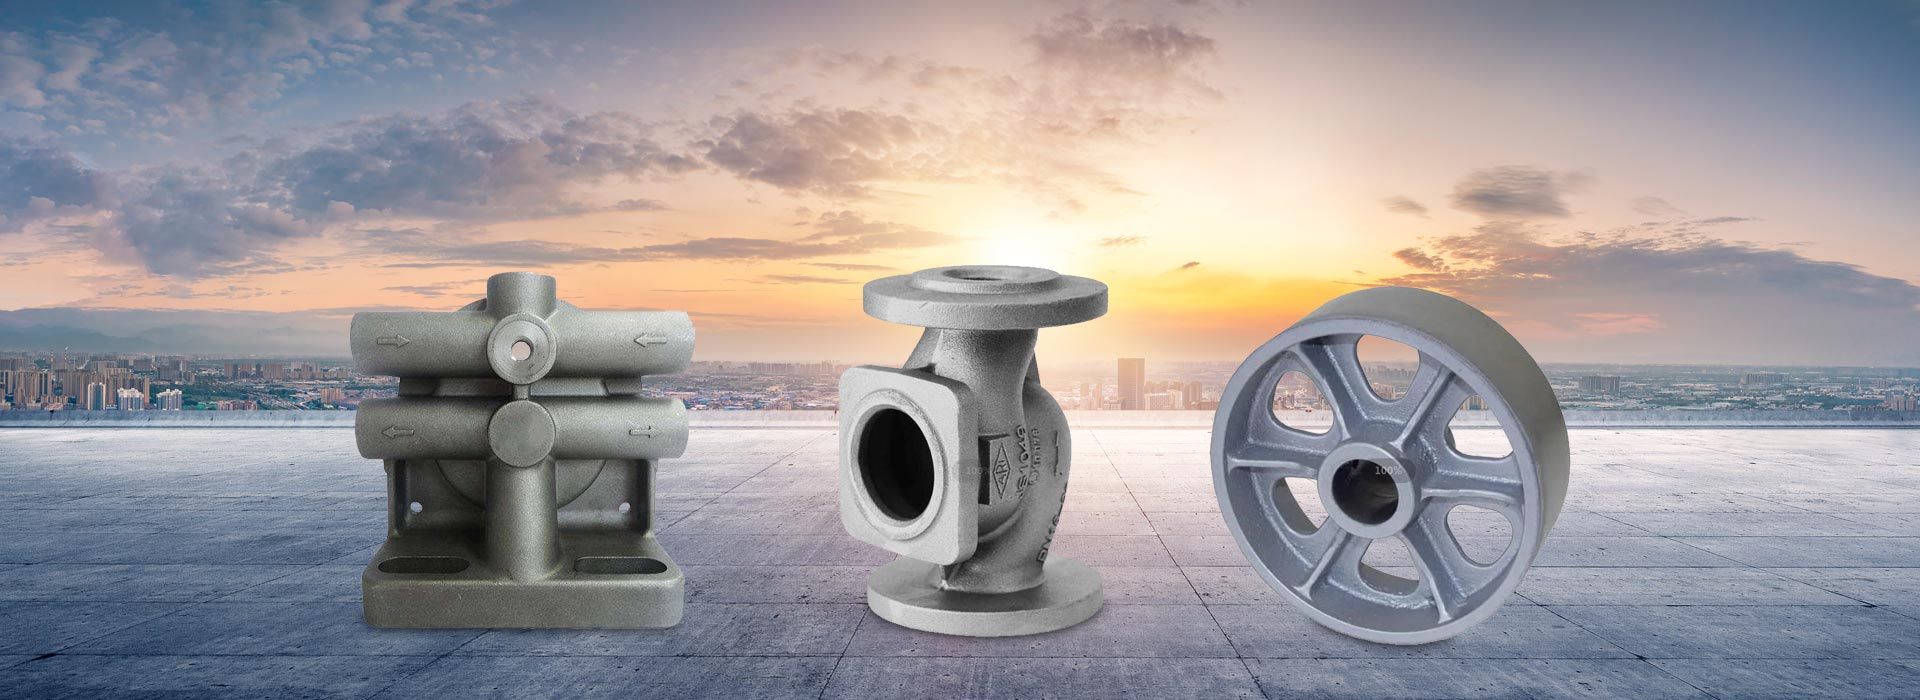
Iron casting strength is rarely the result of a single breakthrough—it comes from how a foundry manages every detail between molten metal and final component. At Supreme Machinery, those details are treated as process controls, not guesses. This post walks through the core factory stages that consistently deliver iron parts with the load-bearing performance demanding applications require.
The Pouring Speed That Shapes Internal Soundness
Pouring speed rarely gets the attention it deserves. Most foundry discussions focus on temperatures or alloy chemistry, but the rate at which metal enters the mold quietly decides whether a casting will hold pressure or hide porosity in its thickest sections. Too fast and the metal churns, trapping air and oxides; too slow and the front begins to freeze before the cavity fills. Internal soundness is shaped in that narrow window.
A steady, controlled pour gives the metal time to push gases ahead of the flow instead of swallowing them. When speed is matched to section thickness and mold venting, the solidification front stays more orderly, and shrinkage tends to draw from risers rather than from the middle of the casting. Operators who adjust pouring speed by watching the sprue and listening to the mold often catch problems that a fixed recipe misses.
The practical goal is not a single perfect number but a repeatable range for each part geometry. Changes in pouring speed can shift the location of last-solidified zones, so internal defects may move rather than disappear. That is why trials should include sectioning or radiographic checks, not just surface appearance. When speed is treated as a process variable instead of a habit, internal soundness becomes easier to hold lot after lot.
Why Controlled Shakeout Matters More Than It Seems
A controlled shakeout often looks like a minor cleanup step, but it quietly decides whether a startup keeps its footing or slides into chaos. When founders rush to cut costs across the board, they rarely notice how much operational memory disappears with each departure. The difference lies in which roles you trim and how you preserve the informal knowledge that keeps daily work moving.
Teams that handle shakeouts poorly tend to lose exactly the people who knew why certain systems existed in the first place. That loss rarely shows up on a spreadsheet, but it surfaces weeks later as slower decisions, repeated mistakes, and a growing sense that nobody remembers the original logic. A controlled approach, by contrast, treats the reduction as a design problem: you identify which functions can pause without breaking customer trust and which ones must stay intact even if they look expensive.
What often gets overlooked is the psychological signal a shakeout sends to those who remain. Haphazard cuts breed anxiety and encourage the best performers to start looking elsewhere. A deliberate, clearly communicated reduction can do the opposite: it shows that leadership understands the real value drivers and is willing to protect them. That clarity is worth far more than the immediate cost savings, because it determines whether the team rebuilds with confidence or merely survives the quarter.
Molding Sand That Holds a Tolerance Others Lose
A molding sand that drifts under heat will quietly undo even the tightest pattern work. This blend is built around a tightly graded sand base, so thermal expansion stays uniform instead of twisting the cavity during the pour. The result is a mold that reads the same after the metal cools as it did before the flask was closed.
The bond package is lean but stubborn. It releases cleanly without crumbling at the edges, and it holds sharp corners long enough to avoid the usual washout where thin sections meet heavier metal. Operators notice it most when the shakeout is fast and the casting still carries the original dimensions.
Day after day, that consistency shows up in fewer mismatches, less stock left for machining, and patterns that do not need constant rework. The tolerance is not promised on a data sheet; it is held in the sand itself.
Alloying Choices Made Before the Furnace Peaks
Walking the melt deck before the first charge hits the roof of the furnace, the decisions that matter most are already locked in the scrap pile and the alloy bins. A late change in silicon or copper isn't just a tap tweak; it reshapes how the slag moves, how the bath temperature climbs, and whether the final chemistry will hold the grade without an expensive trim. Old hands read the pile the way a baker reads dough, checking for heavy plate, turnings, and tramp elements that can hide in a load nobody inspected twice.
The real skill is knowing which alloys can wait and which ones must ride with the first bucket. Carbon, manganese, and chromium often behave if they join early, given time to dissolve and mix before oxygen blows through. Meanwhile nickel and molybdenum like a quieter entry, slipped in after the violent boil settles, so they don't end up stranded in the slag or unevenly scattered through the heat. Each choice changes the arc pattern, the refractory wear, and the way the furnace sounds as it approaches peak power.
No two shops make these calls the same way, and that's the point. A coastal mill with wet turnings might push silicon harder than an inland plant running clean busheling. A night shift foreman may ignore the written recipe and drop half the chrome into the second bucket because he knows his transformer can't take the full load early. Those small departures, repeated and refined, become the invisible edge that separates a smooth heat from one that fights the clock all the way to the tap.
A Cooling Path Designed Around the Thickest Section
Treating the thickest section as the thermal centerline changes how a cooling layout comes together. Instead of placing channels at uniform spacing and hoping the mold temperature evens out, the circuit is routed so coolant reaches the heaviest mass first. The channel depth, diameter, and flow rate are then stepped down in lighter regions, which keeps the core from acting as a heat sink that distorts the part.
That early concentration of cooling only works if the thick area is not overcooled at the surface. A thick wall can shed heat quickly at the skin while the center stays molten, so the path needs dwell zones or angled branches that hold extraction long enough to pull energy from the middle without freezing the gate or the cosmetic surface. In practice this often means reducing linear velocity through the heavy section rather than adding more circuits.
Validation usually comes from short shots and thermal imaging, not just simulation. The telltale sign of a well-placed path is a gradual shift in gloss or texture rather than a visible boundary line around the thick zone. Small adjustments to the return-side diameter or the use of baffles inside deep cores can shift that balance enough to remove sinks and warpage without lengthening the cycle.
Proof Testing That Mimics Real Load, Not Just Lab Conditions
Most bench tests fail because they treat conditions as separate, static values. A power supply gets baked in an oven, shaken on a shaker, or cycled in a humidity chamber, but never all at once. Real equipment in the field sees temperature swing while vibration is hammering connectors and load current is spiking. Proof testing that matters starts with a measured load profile from actual use, not a generic datasheet envelope.
The test rig needs to reproduce that chaos. Instead of a fixed resistor bank, use programmable loads that follow recorded current traces. Add thermal shock, not just steady-state heat, and overlay vibration spectra captured from mounting points on a running machine. The goal is to find the weak solder joint, the marginal capacitor, or the connector that walks loose when everything peaks at the same time. That is the kind of failure a clean lab bench rarely exposes.
Done well, this approach shortens the gap between qualification and warranty claims. A proof test under realistic combined stress is not about pass/fail theater; it gives engineering a repeatable way to trigger and then fix failure mechanisms before units ship. If the test setup does not make you a little uncomfortable, it probably is not mimicking the real load closely enough.
FAQ
Foundries use chills against the mold wall and size risers so the last liquid to solidify sits where it can still feed the casting. That prevents isolated hot spots from turning into shrinkage voids, especially in sections where two walls meet.
A lower pouring temperature reduces mold erosion and sand burn-on, but only works when the metal chemistry and gating are tuned for fluidity. The benefit is a cleaner surface and less gas pickup, so the finished part has fewer sites where cracks can start.
It introduces fine nuclei that push the carbon into small, evenly distributed graphite flakes or nodules instead of coarse or carbidic forms. A well-inoculated melt holds that structure long enough to fill thin sections, which gives more consistent hardness and tensile strength across the part.
In a rigid mold, the expansion of graphite during solidification presses back against the casting and helps feed remaining liquid into areas that would otherwise shrink. Softer molds let the cavity swell and leave microporosity, which lowers density and fatigue resistance.
It cannot remove gas holes or slag inclusions, but it can reshape the metal matrix. Normalizing, annealing, and austempering shift the balance between pearlite and ferrite or create acicular structures, which changes tensile strength, elongation, and impact behavior without altering the casting shape.
They pour test bars from the same ladle and monitor ultrasonic velocity or resonant frequency as a proxy for modulus and soundness. Brinell hardness readings and periodic metallographic checks of graphite shape then tie those nondestructive results back to expected tensile properties.
The difference usually comes from tighter raw material sorting, real-time thermal analysis before pouring, filtered and bottom-pour ladle practice, in-stream inoculation, rigid tooling, and simulation of filling and solidification before the first mold is made.
Conclusion
The strength of an iron casting rarely comes from a single dramatic step. It is set early, when the alloy addition is trimmed before the furnace reaches full temperature, and again during pouring, where a controlled fill rate prevents turbulent metal from folding oxides into the body. The result is a casting whose internal soundness holds up under machining rather than exposing scattered porosity. Cooling is treated as part of the design, not an afterthought: the slowest path is deliberately routed through the thickest section so that the last metal to freeze feeds the areas most likely to shrink. That keeps residual stress from concentrating where section changes meet.
Dimensional control depends on molding sand that stays consistent enough to hold a tolerance across long runs, not just on a first sample. After solidification, the shakeout is timed and controlled; knocking the casting out too hot or too violently can introduce fine cracking that later gets blamed on design. Finally, proof testing loads the component in the same way it will be loaded in service, with instrumentation placed at the highest-strain locations rather than on a generic test bar. Each step works together, and that sequence is what gives the finished part its dependable strength.
Contact Us
Contact Person: Paul
Email: [email protected]
Tel/WhatsApp: 8615067447509
Website: https://www.spironcasting.com