High Quality Mid-Diameter Fiber Fusion Splicer A Complete Buying Guide
2026-08-28
Most buying guides for mid-diameter fiber fusion splicers read like a spec sheet with extra steps. That doesn't help when you're standing in a dusty enclosure or racing a service window. So we took a different approach: start with the failures, the hidden costs, and the small design choices that only show up after weeks of daily use. Whether you're comparing electrode life, heating time, or splice loss consistency, the right machine changes how your crews work. And if you're looking for a brand that doesn't treat durability as an afterthought, DVP deserves a closer look. Let's get into what actually makes a high-quality mid-diameter splicer worth buying.
What Mid-Diameter Actually Means for Your Splice Quality
Mid-diameter is the measured cladding diameter of a fiber, typically close to 125 µm, but no two fibers are exactly alike. When you splice two fibers with different mid-diameters, the cladding alignment your splicer relies on can push the cores off-center relative to each other. That offset, even a fraction of a micron, becomes a direct source of insertion loss and back reflection in the finished splice.
The problem is more pronounced with single-mode fiber because its core is only about 9 µm wide. A mid-diameter difference of just 1 µm can create a core misalignment that exceeds typical loss budgets for high-quality splices. If your splicer aligns on cladding edges, it assumes the cores are perfectly centered in the cladding. Fibers with off-center cores or inconsistent cladding diameters break that assumption, and the splice quality drops without any warning during the alignment process.
Checking the actual mid-diameter before splicing lets you group fibers with similar dimensions or adjust the splicer’s alignment offset. Some splicers allow you to enter known diameter values or use core alignment modes that rely on visual core detection instead of cladding edges. For consistent results, it is worth measuring and tracking mid-diameter on critical links, because a small improvement in offset control often translates into noticeably lower loss and fewer field rework events.
Core Alignment vs. Cladding Alignment: Which One Earns Its Price?
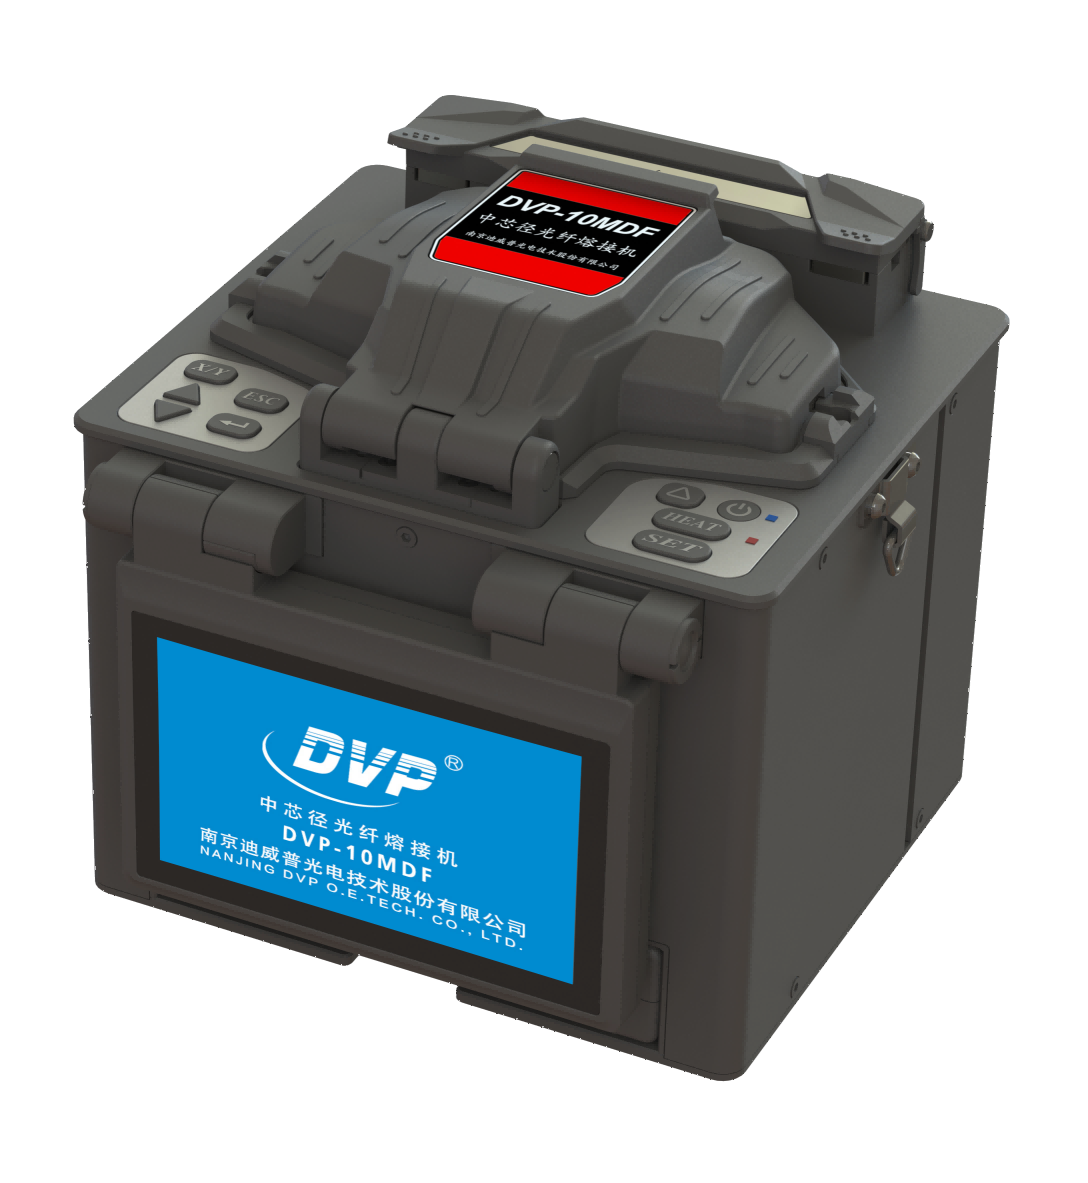
When fiber optic installers talk about alignment, they're usually referring to two very different beasts: core alignment and cladding alignment. Core alignment machines line up the actual light-carrying cores of two fibers—often down to a fraction of a micron—using sophisticated imaging and motorized stages. Cladding alignment takes a simpler route, matching the outer diameter of the glass instead. The difference shows up in splice loss numbers: core alignment consistently hits 0.02 dB or lower on single-mode fiber, while cladding alignment might land anywhere from 0.05 dB to 0.1 dB depending on core concentricity errors in the fiber itself.
But does that tighter splice really justify the jump in price? A top-tier core alignment splicer can cost three to five times more than a solid cladding alignment model. If you're working with legacy multimode fiber or doing quick repairs in less demanding environments, that extra precision often never gets used—the fiber's own geometry variations make core alignment's theoretical advantage moot. On the other hand, for long-haul single-mode links, dense WDM systems, or any network where every tenth of a decibel eats into your power budget, core alignment pays for itself after the first few hundred splices by avoiding costly rework and link failures.
The real question isn't which alignment method is better, but which one matches your actual splicing volume and fiber type. Many contractors buy the most expensive core alignment splicer they can afford, only to discover that cladding alignment would have handled 90% of their jobs without complaint. Look at the fibers you actually splice, check the manufacturer's core-to-cladding concentricity specs, and calculate your average loss margin. That's how you earn the price—not by chasing a spec sheet on a machine you'll never push to its limits.
The Hidden Cost of Cheap Electrodes and Short Lifespans
Budget electrodes might look like a win on the purchase order, but their true price shows up months later. When tips wear down or coatings flake after a few hundred cycles, the real expense isn't the replacement part—it's the unscheduled downtime, the scrapped batches, and the overtime hours spent troubleshooting drift that should never have happened.
Short lifespans also quietly warp your process data. Operators learn to compensate for unstable readings by tweaking settings more often, which masks gradual sensor decay and leads to inconsistent product quality. Before long, you're not just paying for more electrodes; you're paying for rework, customer returns, and a calibration schedule that no longer matches actual performance.
The smart comparison isn't unit price versus unit price. It's total cost per reliable measurement hour. A slightly pricier electrode that holds its slope and zero point for twice as long often eliminates entire maintenance shifts and yields a lower true operating cost—even before you factor in the trust your QA team regains in the numbers.
Field-Ready Features That Matter More Than Spec Sheets
A rugged device lives or dies by how it behaves when the weather turns ugly, not by how many cores its processor has. You might glance at a spec sheet and see an IP68 rating, but that tells you little about whether the screen stays readable under direct sun, whether the charging port survives repeated exposure to salt spray, or whether the buttons remain usable with thick gloves on. These are the details that field technicians, surveyors, and emergency responders learn to prioritize after a single season of real-world use.
Battery life is another area where paper numbers mislead. A manufacturer can claim a 5,000mAh cell, but if the device burns through it in six hours because of poor power management or a hot-running radio, that spec means nothing. In the field, you need a device that can survive a full shift, maybe two, without hunting for an outlet. Hot-swappable batteries often matter more than fast charging, because you can't always pause work to sit next to a charger.
Connectivity also separates field-ready gear from consumer toys. A device that drops its signal every time you walk behind a concrete wall or enter a basement is useless for inspections or search and rescue. Look for models with external antenna ports, support for multiple carrier bands, and a track record of holding a connection in fringe areas. These are the features that never make the front of a brochure, but they are the ones that save you from walking back to the truck to re-download a map.
How to Test a Splicer Before You Pay for It
Start by asking the seller to perform a live demonstration on the exact fiber types you plan to use. Watch how the splicer aligns the cores, whether it shows clear magnification on the screen, and how many splices it takes before the estimated loss drops below 0.03 dB. A machine that needs constant manual adjustment or produces wildly inconsistent loss readings will cost you more in rework than you save on the purchase.
After the demo, run your own test splices if the seller allows. Pay attention to the cleaver and stripper: dull blades or misaligned clamps are a red flag. Check the electrode condition by opening the wind cover and looking for pitting or carbon buildup—replacement electrodes aren’t cheap, and they wear out faster if the previous owner ran the arc too hot. Also test the heater oven with a couple of splice protectors to confirm it reaches temperature and doesn’t crack the sleeves.
Finally, plug the splicer into a power meter or OTDR and measure the actual loss of a splice, not just the machine’s estimate. Do this on both single-mode and multimode fiber if you work with both. If the seller can’t or won’t let you run these checks, treat that as a warning sign. A splicer that passes a thorough hands-on test will save you from buying someone else’s worn-out workhorse.
Maintenance Habits That Keep a High-Quality Splicer Running
A quality splicer doesn’t demand constant attention, but it does reward a few consistent habits. Before each shift, take ten seconds to wipe down the V-grooves and fiber clamps with a lint-free cloth dampened in isopropyl alcohol. Many operators skip this step, then wonder why splice losses creep upward. The truth is, microscopic dust and gel residue build up faster than you’d expect, and once they settle into the alignment mechanism, you’re looking at a service call instead of a quick clean.
Battery care often gets overlooked until the pack dies mid-job. Lithium-ion cells don’t like sitting at full charge for weeks, nor do they appreciate being run down to zero. If you’re not using the splicer daily, store the battery around 50% charge in a cool, dry place. When you do charge it, avoid leaving it plugged in overnight after it hits 100%. A little discipline here extends pack life by years, saving you from sudden power loss on a tower or in a trench.
Finally, run the built-in self-calibration routine at least once a month, even if the machine seems fine. Arc intensity drifts with electrode wear, and the firmware can compensate only so far before splices start failing. Keep a spare pair of electrodes in your kit and change them when the calibration warns you—don’t push them past their rated arc count. These habits take minutes, but they keep a high-quality splicer behaving like new long after the warranty expires.
FAQ
Mid-diameter typically covers cladding diameters from roughly 200 µm to 400 µm, though some users include 500 µm. Standard splicers are tuned for 125 µm glass, so their v-grooves, clamps, and imaging systems often cannot center or align larger fibers properly. That leads to core offset, poor loss readings, or even cracked fiber when the clamps close too tightly.
Core alignment gives better geometric matching when the core is not perfectly centered in the cladding, which happens more often in specialty and mid-diameter fiber. Cladding alignment can work if the fiber has tight concentricity tolerances, but for demanding applications like medical laser delivery or high-power sensing, core alignment is usually worth the extra cost because it directly targets the light path.
Look for wide-range v-grooves or interchangeable fiber holders, motorized clamps with adjustable pressure, a high-resolution dual-axis viewing system, and software profiles designed for larger diameters. A true mid-diameter unit will also let you store custom parameters for different fiber types instead of forcing a one-size-fits-all recipe.
Yes, if the machine has quick-change holders or a tool-free clamp system and clearly separated calibration profiles. Switching should take under a minute per side. However, you will still need to clean the v-grooves and verify the arc calibration when moving between very different diameters to avoid drift in loss readings.
Bring your own fiber samples and run at least 20 consecutive splices under typical field conditions. Record loss for each splice, then check the standard deviation. A high quality unit should stay below 0.05 dB average for identical fiber and below 0.10 dB for mixed diameters, with no sudden outliers caused by clamp marks or core offset.
Clean the v-grooves and electrodes after every 50 to 100 splices, or more often in dusty environments. Do not use cotton swabs that leave lint. Check electrode condition weekly with the built-in arc test, and recalibrate the imaging system whenever you change fiber holders or notice a shift in loss consistency.
Yes, electrode replacement, specialized fiber holders for non-standard diameters, software upgrades for new fiber types, and a calibration service contract all add up. Factor in a carrying case with good shock protection if you work in the field, because misalignment from a single drop can cost more than the accessory itself.
Conclusion
When you're splicing mid-diameter fiber, the first thing to realize is that "mid-diameter" isn't a marketing label—it changes how the machine grips, strips, and aligns every single strand. A splicer that merely clamps a 200 μm or 250 μm fiber without adjusting its V-groove or mirror geometry will produce excessive loss, especially on long-haul or sensing links. That's why you should check whether the unit's core alignment system actually images the core rather than just assuming the cladding is concentric. Core alignment costs more up front but pays for itself the first time you avoid rework on a buried cable. Meanwhile, cheap electrodes are the easiest way to ruin a bargain splicer: they wear unevenly, create unstable arcs, and force you to replace them twice as often. A reputable machine uses dense, slow-wearing electrodes and tracks arc count so you can plan replacements instead of discovering a failure mid-splice.
Beyond bench specs, look for field-ready details that don't appear on data sheets: a sealed screen readable in direct sunlight, a windproof hood that actually closes over the splice point, and a battery that lasts through a full workday rather than needing a midday top-up. Before paying, test the machine with your own fiber—watch how it handles slightly dirty or imperfect cleaves, and measure loss on at least ten consecutive splices; consistency matters more than a single perfect number. Once you own it, simple habits keep it performing: clean the V-grooves and mirrors weekly, calibrate the arc after any electrode change, and store the splicer in a dry case with silica gel. Skipping these steps slowly drifts your splice loss upward, and by the time you notice, you've already burned through time and materials on a job that should have been routine.
Contact Us
Contact Person: Mr XU
Email: [email protected]
Tel/WhatsApp: 86-25-85582828
Website: https://www.dvp.cn/en/