Custom SiC Wafer Boat: Essential Design Tips for Optimal Performance
2026-09-26
Designing a custom SiC wafer boat isn't just about copying a standard shape—it's about matching the boat to your exact thermal budget, wafer size, and handling setup. Many engineers discover too late that off-the-shelf options compromise yield or lifespan. At Semicorex, we're sharing the design principles that separate high-performance carriers from costly failures. Here's what to prioritize before you commit to a prototype.
Material Selection Beyond Silicon Carbide: What Actually Holds Up
Silicon carbide's dominance in high-temperature, high-voltage power electronics isn't unearned, but plenty of teams now look for alternatives that don't just match its specs on paper. Gallium nitride keeps proving itself in fast-switching, medium-voltage applications where efficiency wins matter more than raw thermal headroom. Yet the real gauge is whether a material holds up after thousands of hours of thermal cycling, not in a single lab demo.
Then there's diamond, which sounds like a punchline until you check its thermal conductivity. The catch is that growing device-grade diamond at wafer scale is still brutally expensive, so it stays confined to niche RF and high-power optical windows. Meanwhile, beta-phase gallium oxide has become the quiet contender for next-gen power diodes because its bandgap outpaces SiC while the substrate cost is theoretically lower. But defect control and p-type doping remain unsolved, and that keeps it from leaving the research phase.
One thing gets overlooked: packaging and metallization often kill a material before the semiconductor itself fails. Aluminum nitride and even some engineered ceramics are being pushed as substrates and heat spreaders because they can handle the thermal mismatch better than the chip material alone. If you ignore that layer of the stack, you're not really testing what holds up.
Avoiding Thermal Shock: Boat Geometry That Survives Rapid Cycling
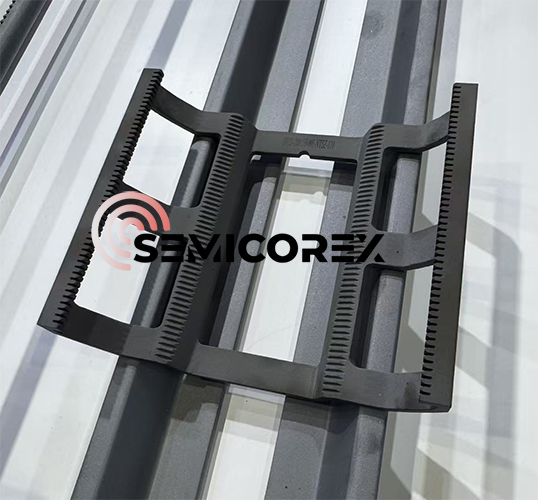
Sharp corners and abrupt thickness changes concentrate stress when a hull heats and cools repeatedly. A fillet radius of at least three times the adjacent plate thickness lets thermal strain redistribute along a smooth path instead of piling up at a single notch. This simple geometric shift often matters more than switching to a higher-grade alloy.
Rapid cycling also punishes asymmetric framing. Staggered stiffeners or uneven spacing between longitudinals create hot spots that lag behind the rest of the structure during a temperature swing. Aligning frames so that each bay expands at a similar rate keeps the hull from bowing inward or cracking at weld toes. Designers who taper plate thickness over a span rather than stepping it down abruptly buy extra fatigue life for very little added weight.
Testing these shapes under realistic thermal pulses — not just steady-state heat — reveals where buckling starts. A hull that survives one harsh cycle may still fail after fifty milder ones if local geometry forces repeated plastic strain. Iterating on curvature and frame pitch with rapid cycling in mind turns thermal shock from a failure mode into a manageable load case.
Slot Tolerance and Pitch: The Overlooked Details Behind Wafer Yield
When process engineers chase yield loss, they usually tear into etch profiles, film thickness, or lithography overlay. But a silent contributor often hides in plain sight: the slot tolerance and pitch of wafer handling and storage cassettes. A slot that is just a few hundred microns wider than nominal allows the wafer to shift during transfer, micro-scratching the backside or edge. Those barely visible marks become nucleation sites for particle adhesion, and by the time they reach the litho cell, the damage is already done.
Pitch errors between adjacent slots create a different failure mode. If one slot sits slightly off the nominal centerline, the end effector may contact the wafer at a slight angle, introducing a torque that warps the wafer or causes it to vibrate during high-speed moves. Over thousands of cycles, this cumulative stress leads to slip lines in the crystal lattice, especially near the edge exclusion zone. The result is a yield pattern that looks random on wafer maps but correlates perfectly with cassette position when analyzed properly.
What makes these details so dangerous is their invisibility in standard metrology. A cassette can pass incoming inspection with all slots within a generous tolerance band, yet fail in production because of pitch variation that only appears under thermal load. Wafer fabs that treat cassette slot geometry as a consumable spec rather than a process variable are essentially gambling with their baseline yield, and the losses show up as mysterious edge die failures that no amount of recipe tuning can fix.
Surface Roughness and Coatings: Preventing Particle Generation at Temperature
The link between surface roughness and particle shedding becomes far more pronounced when components are heated. At room temperature, a machined or polished surface may seem stable, but thermal cycling introduces differential expansion between the bulk material and any surface irregularities. Peaks and troughs on the rough surface expand unevenly, and the resulting stress can fracture microscopic asperities, releasing them as airborne particles. In high-temperature process environments— whether inside a furnace, a deposition chamber, or a hot gas line—those loose particles can contaminate wafers, optics, or sensitive coatings. Reducing roughness below a certain threshold, typically measured in Ra or Rq, minimizes the number of vulnerable high points that can snap off during heating.
Coatings play a dual role in this scenario. A dense, well-adhered coating can smooth over the substrate’s rough profile, filling valleys and covering sharp peaks, which lowers the effective surface roughness without requiring extensive mechanical polishing of the base material. More importantly, the coating itself must be thermally stable and matched to the substrate’s coefficient of thermal expansion. If the coating expands at a very different rate than the underlying metal or ceramic, microcracks can form at the interface after repeated heating and cooling. Those cracks act as new particle sources. Hard ceramic coatings like aluminum oxide, silicon carbide, or yttria-stabilized zirconia are often chosen for high-temperature service because they combine low roughness after deposition with resistance to oxidation and spalling.
Material selection alone does not guarantee particle-free performance. The coating’s thickness, deposition method, and post-coating surface finish all influence how it behaves at temperature. A thin film applied by chemical vapor deposition may conform to the substrate roughness, preserving some of the original texture, while a thicker thermal spray coating can be ground and lapped to an extremely smooth finish. After thermal cycling, it is essential to re-measure roughness and inspect for delamination or pinholes, because even a few microns of exposed substrate can become an oxidation site that sheds debris. In practice, preventing particle generation at temperature is less about a single perfect solution and more about matching the right coating architecture to the expected thermal range and surface quality requirements.
Designing Out Contamination: Hidden Sources of Doping and Defects
Most contamination control plans spend their energy on the obvious—dirty cassettes, exhausted filters, or a thumbprint on a wafer edge. But the hidden sources of doping and defects usually enter through the supply chain itself. A phosphine or arsine cylinder can carry trace moisture, metal carbonyls, or oxygen that never show up on a standard certificate of analysis. Once those impurities reach the chamber, they alter activation ratios, shift threshold voltages, and create deep-level traps that only surface as random yield loss weeks later.
Hardware choices matter just as much as chemistry. Quartz ware, graphite fixtures, and elastomer seals all look inert on a shelf, yet under plasma or high-temperature cycling they outgas, sputter, or slowly release iron, nickel, and copper. These metals diffuse fast enough to kill minority carrier lifetime in a single thermal step. Designing them out means specifying materials by their actual trace-metal content and testing each new part number under process conditions—not assuming that a clean-looking surface is a clean surface.
Defects are also designed in by the thermal and wet processes themselves. Rapid temperature ramps across a wafer with uneven emissivity create slip and stacking faults. Wet benches leave organic films that later turn into interfacial traps or fixed oxide charge. The shift that works is to make contamination geometrically or chemically impossible: shorten gas lines, pre-condition chambers with sacrificial runs, replace aqueous cleans with vapor-phase alternatives where you can. Prevention, not inspection, is what finally removes those recurring ghost defects from the line.
Balancing Load Size and Heat Uniformity for Consistent Results
Most thermal processing setups run into trouble when the chamber is either too empty or packed to the edges. A sparse load lets heated air or radiation move too freely, causing the controller to cycle more often and producing uneven surface temperatures, while a dense load blocks circulation and leaves the center of the batch noticeably behind the edges.
Finding the right fill level usually means leaving enough gaps for the heating medium to wrap around individual pieces. For tray-based systems, spacing items at least a finger-width apart often works better than trying to maximize capacity in a single run. If you have to run dense loads, adding a mid-cycle rotation or shifting trays between levels can correct much of the lag that builds up in the middle.
Consistency across batches comes from treating the load size as a variable you control, not a given. Keep a simple log of how full the chamber was, where you placed the largest pieces, and what the final result looked like, then adjust the next cycle by one or two items at a time. Over a few runs you will find a sweet spot where the load is full enough to be efficient but open enough for heat to reach every surface at roughly the same rate.
FAQ
Start with wafer diameter, pitch, and the exact furnace zone profile. These set the boat's outer envelope, slot count, and how the mass is distributed along the heating length. If you skip this step, even a perfectly machined boat will struggle with temperature ramping or robotic handling.
Slot depth, width, and edge chamfer all change how wafers see radiant heat from the elements. A deeper slot shields the wafer edge but can create a cooler rim, while a shallow slot improves direct heating but reduces grip. The best designs use a slight taper or rounded bottom to keep wafers centered without creating a thermal shadow.
Fine, uniform grain size limits micro-cracking from repeated thermal cycling, and high purity prevents metallic contaminants from vaporizing onto wafers during processing. For LPCVD or oxidation tubes, even trace iron or nickel can ruin device yield, so custom boats should specify sintered alpha-SiC with controlled impurity levels.
Avoid sharp internal corners where debris can collect, use polished contact surfaces, and include generous radii on all machined edges. A smooth, non-porous surface finish below 0.8 µm Ra reduces particle adhesion. For cantilever boats, add small drain slots in the base so any loose particles fall away instead of being carried into the hot zone.
Thicker rails and longer support ribs increase strength but also slow down ramp rates and raise energy use. A better approach is to reinforce only the high-stress zones, like the cantilever root or the wafer contact points, while keeping the rest of the structure as light as the process allows. Finite element analysis can show exactly where material can be removed without compromising load capacity.
Slotted boats work best for high-volume processing where robotic loading speed matters and slight wafer movement is acceptable. Grooved or pocket-style boats hold wafers more securely and reduce contact area, making them better for thin wafers, high-stress films, or processes with strong gas flow. If your furnace has vibration or fast push-pull cycles, a pocket design usually wins.
For cantilever systems, concentrate stiffness in the mounting end and taper the free end to reduce deflection at temperature. For vertical furnaces, center the boat's mass on the tower axis and use symmetric slot patterns to avoid uneven thermal expansion. Both cases benefit from a slightly oversized mounting hole or keyway to account for thermal growth without binding.
Sintered SiC can be machined to ±0.05 mm on critical slot positions and ±0.1 mm on overall length, but expect some variation after the first firing. Better shops will do a pre-fire rough machine, then finish machine after sintering to hit tight tolerances. For wafer pitch, keep tolerance within ±0.03 mm if you use automated loaders, otherwise wafers may jam or sit off-center.
Conclusion
Getting a custom SiC wafer boat to perform well comes down to choices that aren't always obvious on the datasheet. First, while silicon carbide is the default, the actual high-temperature survival often hinges on the binder phase or added reinforcements—some blends handle rapid thermal cycling far better than pure sintered SiC. You also need geometry that doesn't fight the furnace: thinner walls, rounded internal corners, and slotted stress-relief cuts let the boat expand and contract without cracking. Then there's slot tolerance and pitch, which get surprisingly little attention. If slots are cut too tight, wafers bind during heating; too loose, they tilt and create edge contact. Pitch must also match your process tube's gas flow, or you'll see uneven deposition across the batch.
Beyond shape, surface quality and contamination control decide whether your boat helps or hurts yield. As-fired SiC surfaces can shed particles, so a high-temperature CVD coating—often SiC or a densified layer—locks down dust and reduces wafer scratching. But coatings aren't a cure-all: they can peel if the underlying boat was poorly cleaned or if thermal expansion mismatches. Hidden contamination from machining residues, metal traces in the binder, or even outgassing from previous runs can dope wafers or create defects, so specify acid cleaning, high-purity raw materials, and dedicated furnace runs for your boat. Finally, don't ignore the trade-off between load size and heat uniformity. A larger boat holds more wafers, but if its mass shadows the heating elements or blocks gas flow, you'll get edge-to-center temperature gradients that ruin consistency. Sometimes a slightly smaller, better-balanced design gives higher overall yield than pushing wafer count.
Contact Us
Contact Person: Svenja Wei
Email: [email protected]
Tel/WhatsApp: +8613567891907
Website: https://www.semicorex.com